Jiangsu Xindake Connection Technology Co., Ltd. offers you free information and the latest news on battery connectors, battery pack inserts, e-bike battery nickel strips, nickel-plated strips and more. Stay tuned!
Jiangsu Xindake Connection Technology Co., Ltd. offers you free information and the latest news on battery connectors, battery pack inserts, e-bike battery nickel strips, nickel-plated strips and more. Stay tuned!

How can the production efficiency of hardware stamping molds be improved? In the production of hardware stamping molds, the machines need to be maintained and carefully inspected in order to extend their service life. Let's take a look at the maintenance of hardware stamping molds! Precautions.
1. Maintenance of punch and die types
1. When disassembling concave and convex molds, attention should be paid to the original condition of the mold to facilitate restoration during subsequent assembly; if shims or deviations are added, the thickness of the shims should be marked on the parts and properly recorded.
2. When replacing the punch, test whether the stripping block die is inserted smoothly and whether the gap between the insertion and the die is even; When replacing the die, test whether the gap between the insertion and the punch is even.
3. After grinding the punch, if the punch becomes shorter and shims need to be added to achieve the required length, the effective length of the punch should be checked. When replacing a broken punch, the cause should be identified, and at the same time, it is necessary to check whether the corresponding die has chipped edges and whether the cutting edge needs to be ground.
4. When assembling the punch, check whether there is sufficient clearance between the punch and the fixing block or fixing plate. If there is a pressure block, check whether there is any allowance for movement. The die should be placed horizontally when assembling, then use a flat iron block on the die surface and lightly tap it into place with a copper rod. Do not insert it at an angle and strike it forcefully. The bottom of the die should be chamfered. After assembly, check whether the die surface is level with the mold surface.
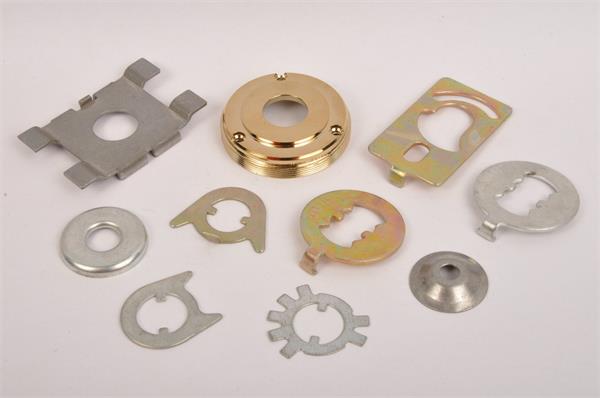
5. After the assembly of the punch, die, and die core, it is necessary to perform the necessary checks against the material strip to see if any parts are installed incorrectly or reversed. Check whether the die and die spacer are installed incorrectly, whether the blanking hole is blocked, whether the newly replaced parts require material stealing, if enough material is stolen as needed, and whether the areas of the mold that need to be locked are secured.
6. Manufacturers of stamped hardware parts should pay attention to confirming the tightening of the ejector plate screws. Tightening should be done from the inside out, with balanced force, and in a cross pattern. Do not tighten one screw first and then another, as this may cause the ejector plate to tilt, leading to punch breakage or reduced mold accuracy.
2. Maintenance of the stripping plate
1. The removal of the stripper plate can first be done by prying it up evenly with two screwdrivers, and then using both hands to apply balanced force to take it out. If difficulties arise during removal, check whether the mold has been cleaned properly, whether all locking screws have been removed, and whether material jamming has caused mold damage. Identify the cause before taking appropriate action, and never handle it blindly.
2. When assembling the stripping plate, first clean the punch and the stripping plate, apply lubricating oil to the guide post and punch entry, place it smoothly, then press it into position with both hands, repeating several times. If it is too tight, the cause should be identified (whether the guiding of the guide post and guide bushing is normal, whether any parts are damaged, whether the newly replaced punch can pass through the stripping plate smoothly, and whether the position is correct), and then take appropriate measures.
3. For fixed plates with pressure blocks, check whether the clearance on the stripper backing plate is sufficient. The contact surface between the stripper plate and the die can develop impressions due to long-term stamping. When the impressions are severe, they can affect the pressing accuracy of the material, causing abnormal and unstable product dimensions. It is necessary to repair or regrind the stripper inserts and the stripper plate.
4. Height-matched sleeves should undergo precision checks; if they are not level, it will cause misalignment of the stripping plate, and its precise guiding and stable spring pressure function will be compromised, requiring maintenance.
Regarding degree and function, replacement is necessary. Check the condition of the stripping spring and the ejection spring to see if they are broken or, although not broken after long-term use, have become fatigued and lost their original strength. Regular maintenance and replacement must be carried out; otherwise, it will cause damage to the mold or disrupt production.
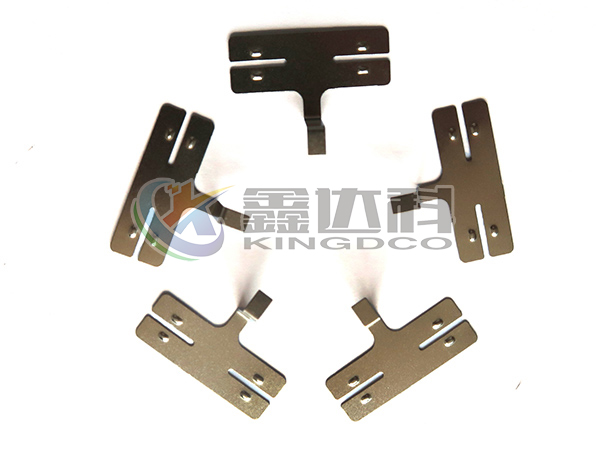
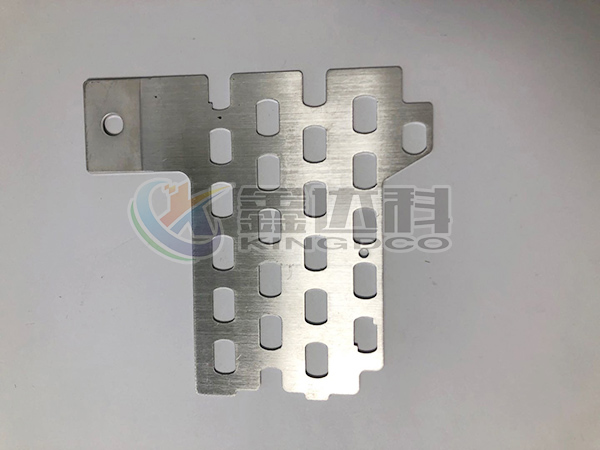
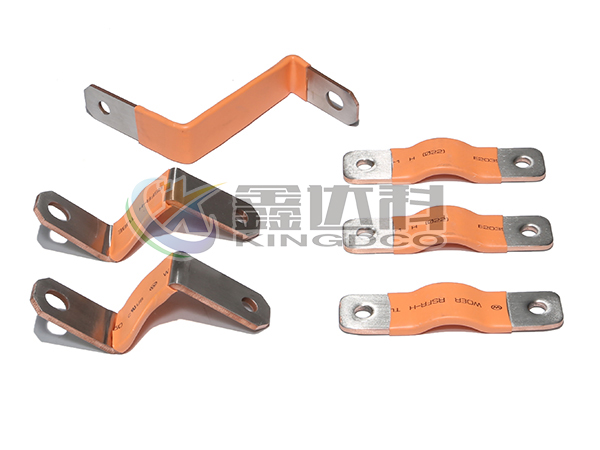
The above is a sharing of the maintenance precautions for hardware stamping progressive dies related to stamping part processing prices. If you want stamping parts, then it is Yixing Xindake New Energy Technology Co., Ltd. Our company specializes in copper foil flexible connectors, copper busbar manufacturing, stamping part processing prices, etc. Thank you for your browsing and support!
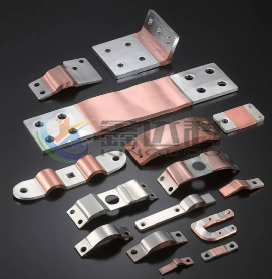
Copper and aluminum busbars are widely used in battery packs. Nowadays, the busbars are mostly made of multilayer copper foil/aluminum foil laminates as the base material, and are fabricated through a...
2026-08-05 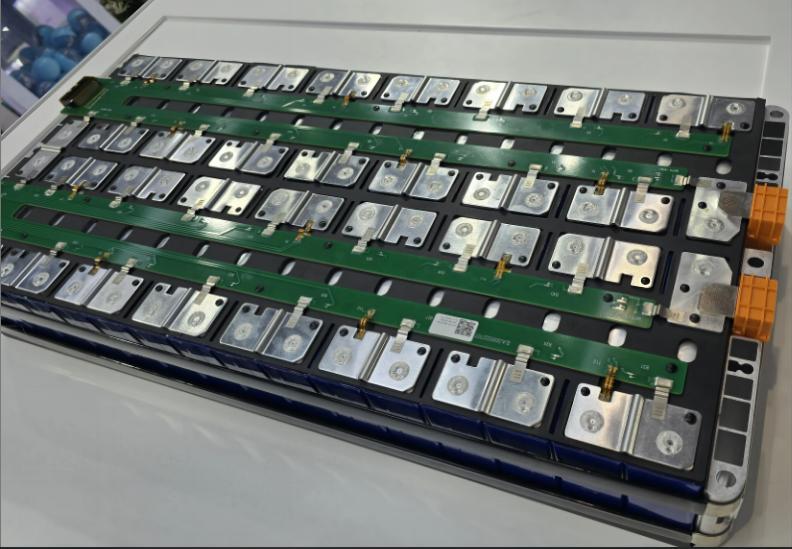
The CCS integrated busbar is mainly composed of signal acquisition components (such as FPC, PCB, FFC, etc.), plastic structural parts, nickel strips, copper busbars, aluminum busbars, etc. These are c...
2025-08-15 
Nickel is a metal with significant industrial value, with a melting point of 1453°C, a boiling point of 3075°C, and a specific gravity of 8.8 g/cm³. It has excellent corrosion resistance, is not easil...
2025-08-15 
Product Name: Power battery soft aluminum busbar, battery module welding flexible connector aluminum busbar, battery soft aluminum busbar Product Material: 1060 O-temper aluminum foil strip, aluminum ...
2023-05-04Phone:
0510-87183933