Jiangsu Xindake Connection Technology Co., Ltd. offers you free information and the latest news on battery connectors, battery pack inserts, e-bike battery nickel strips, nickel-plated strips and more. Stay tuned!
Jiangsu Xindake Connection Technology Co., Ltd. offers you free information and the latest news on battery connectors, battery pack inserts, e-bike battery nickel strips, nickel-plated strips and more. Stay tuned!

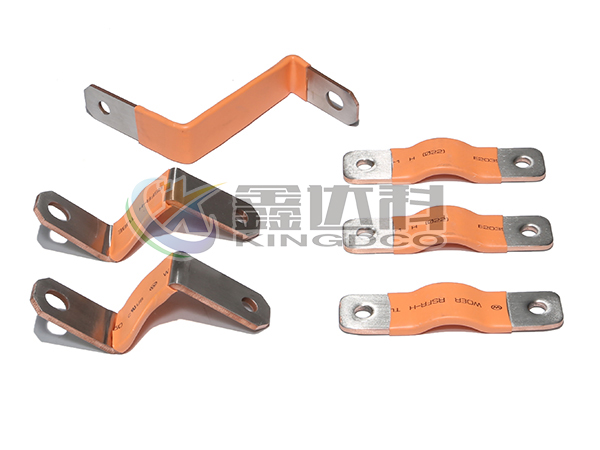
Copper-aluminum flexible busbars are widely used in battery packs. Nowadays, flexible busbars are mostly made from multilayer copper foil/aluminum foil laminates as the base material, and are processed and formed through multiple integrated procedures such as diffusion welding composite, stamping and trimming, and bending and shaping.
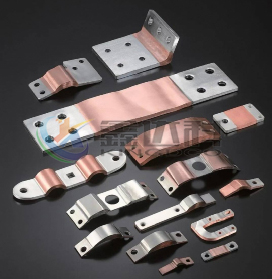
1. Overview of the Production Line
Today we introduce Xindake's soft stranding process solution. The entire standardized production line is divided into eight major processes, relying on diffusion welding core equipment to complete the full process of material compounding, forming, insulation, and inspection.
A single production line occupies about 50㎡, staffed with 6 operators, standard production rhythm is 2 minutes per piece, process is stable and reliable, and the product meets electrical conductivity and mechanical performance standards.
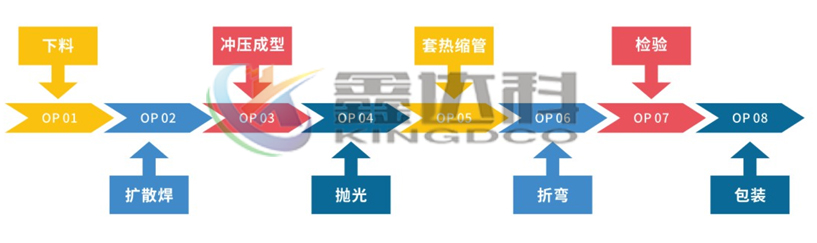
2. Production Process
OP01 Material Cutting:
Material cutting is the first step in production, using a programmable cutting machine to process copper and aluminum coil materials.
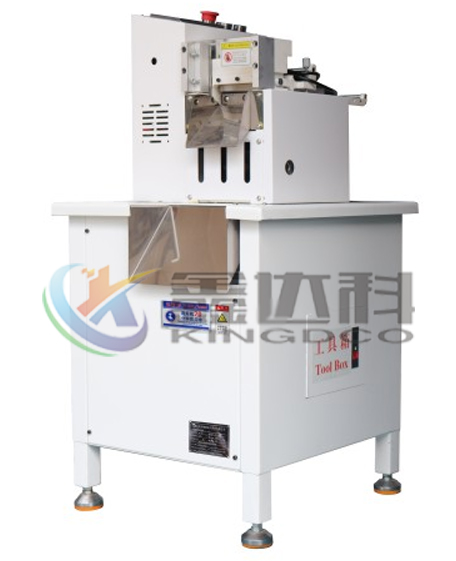
The operator secures the raw material roll on the feeding rack, sets the cutting length and stacking layers according to the product size. The equipment comes with leveling and automatic counting functions, with a cutting accuracy of ±0.1mm and a maximum cutting speed of 80 cuts per minute. The cut single-layer foil is neatly layered and stacked, providing uniformly sized substrates for diffusion welding, with a single workstation production cycle of 5–30 seconds.
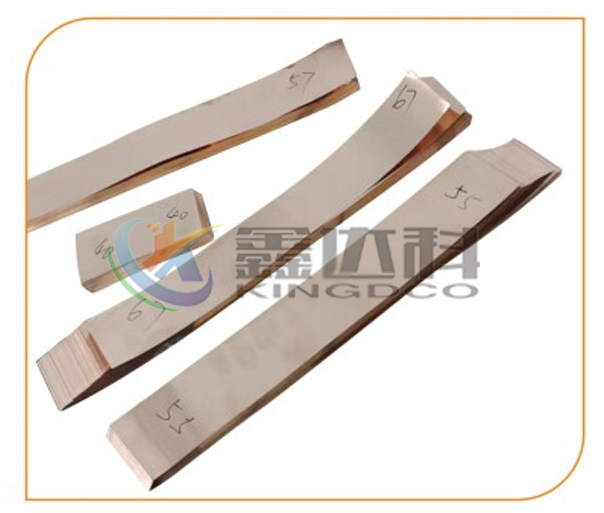
OP02 Diffusion Welding:
Diffusion welding is the core process in soft die forming. Copper materials use a copper welding machine, and aluminum materials are matched with an aluminum welding machine. Both types of equipment feature a C-type servo motor boosting structure, with a maximum output pressure of 10T and a temperature control range of 300~1200°C.
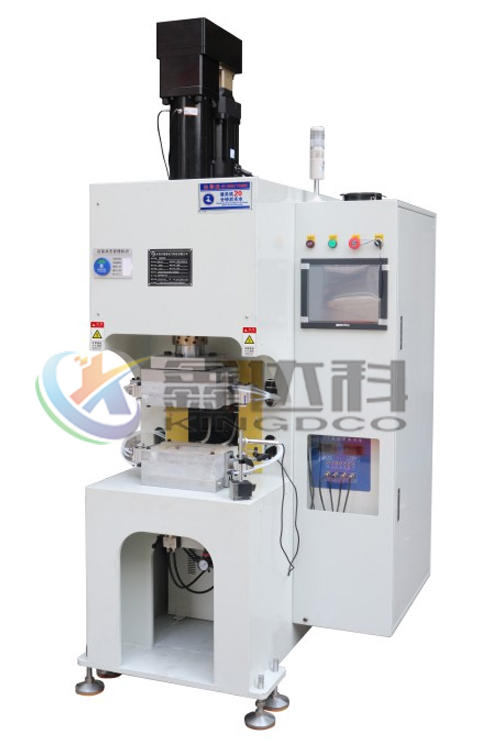
During the operation, multilayer foil materials are positioned and placed on the welding fixture, and the equipment uses variable frequency inversion to precisely control temperature and apply pressure, allowing atoms at the metal interface to permeate each other to achieve a solderless metallurgical bond.
The process strictly controls welding quality, requiring the welded surfaces of the finished product to be smooth and free of bubbles, with no delamination, and the peeling strength and thickness dimensions meeting the requirements.
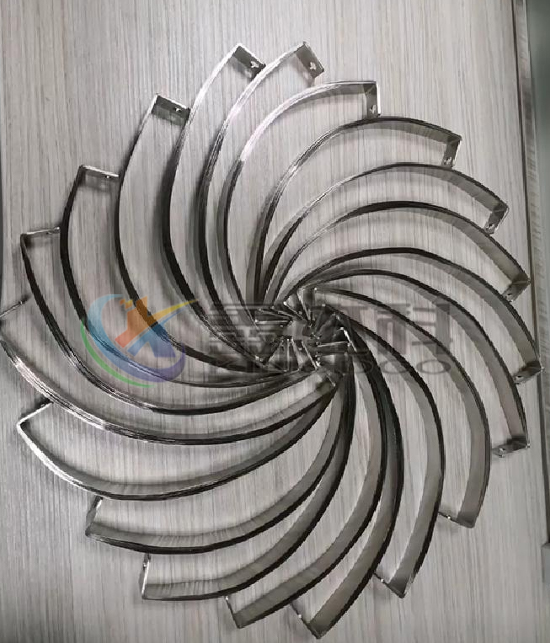
The equipment is equipped with water flow, current anomaly alarm, and infrared safety protection; single welding takes 3~20 seconds, large size products require appropriately longer pressure holding time.
OP03 Stamping Forming:
Stamping uses a dedicated punch to remove excess edges and punch mounting holes from the welded composite soft busbar;
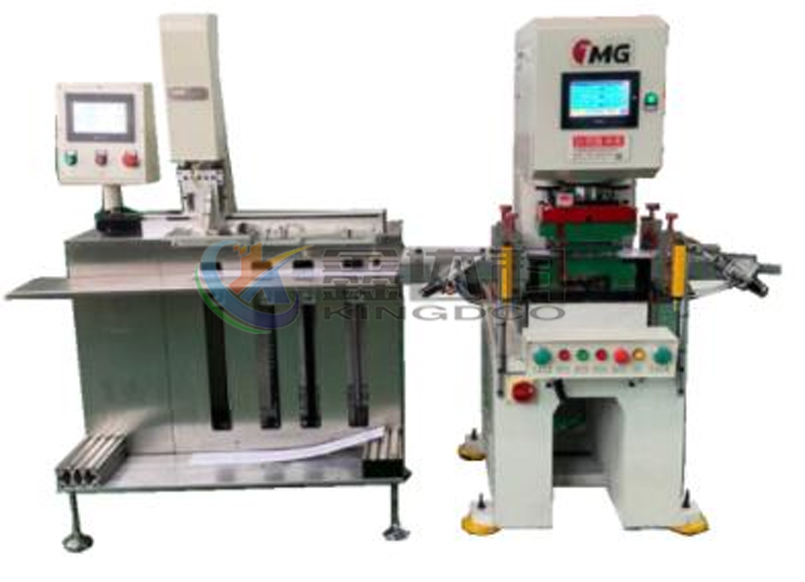
Manual or robotic loading and unloading, the mold completes trimming and punching in one go, finished edges without burrs, surface without pressure marks, cycle time stable at 5 seconds per piece.
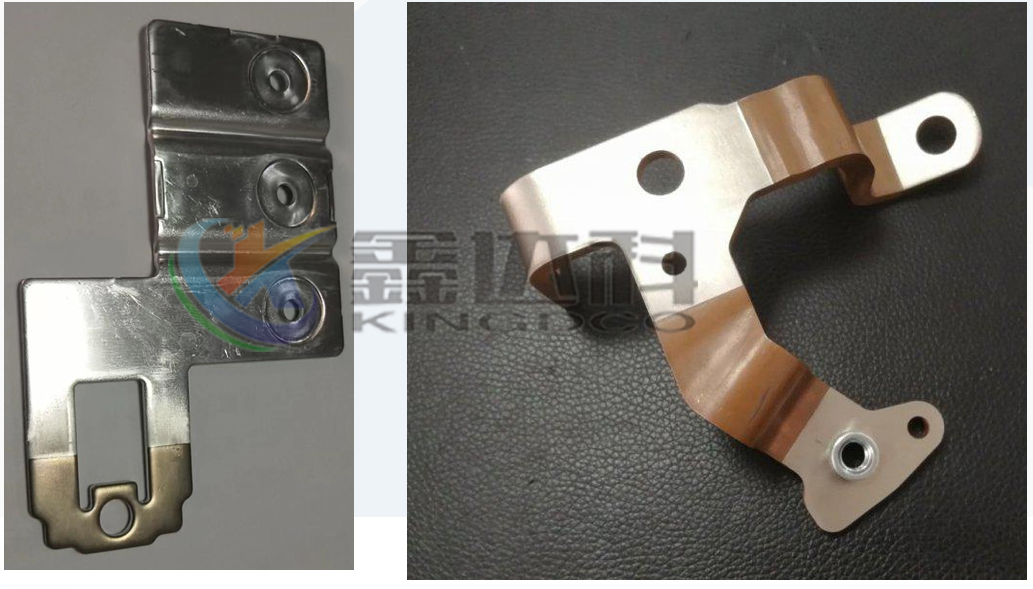
OP04 Grinding and Polishing:
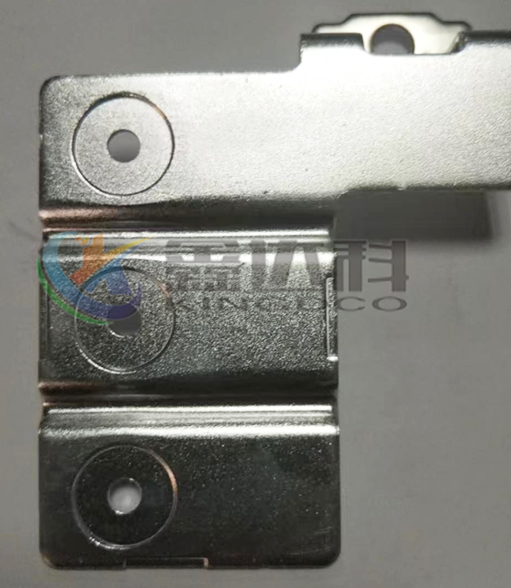
Choose environmentally friendly polishing machines and magnetic grinders, first rough grind to remove the material's oxide layer and surface patterns, then finely polish to smooth out and eliminate machining scratches;
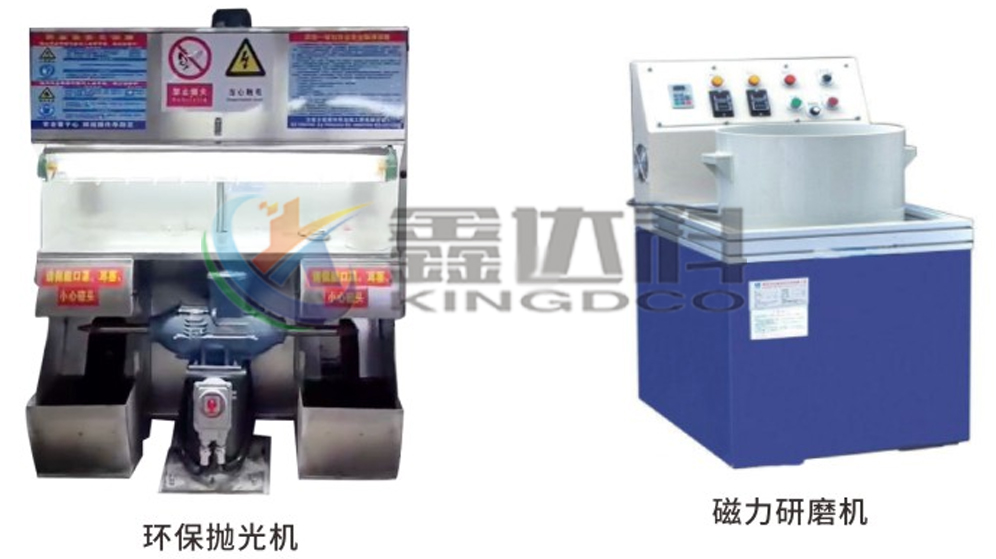
The finished product has a smooth surface without protrusions. Using polishing agents and grinding liquids ensures the treatment effect, and each piece is treated for 5 to 10 seconds.
OP05 Heat Shrink Tube Application:
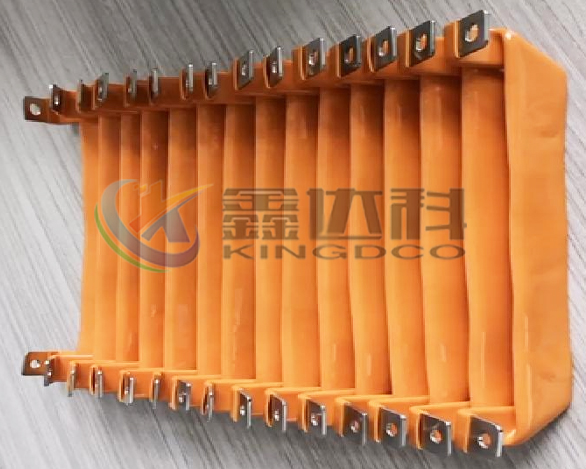
The heat shrink tubing process involves cutting the insulating sleeves with a tube cutter, manually fitting them, and then sending them into a tunnel furnace for high-temperature shrinking to ensure the tubing fits without wrinkles or damage;
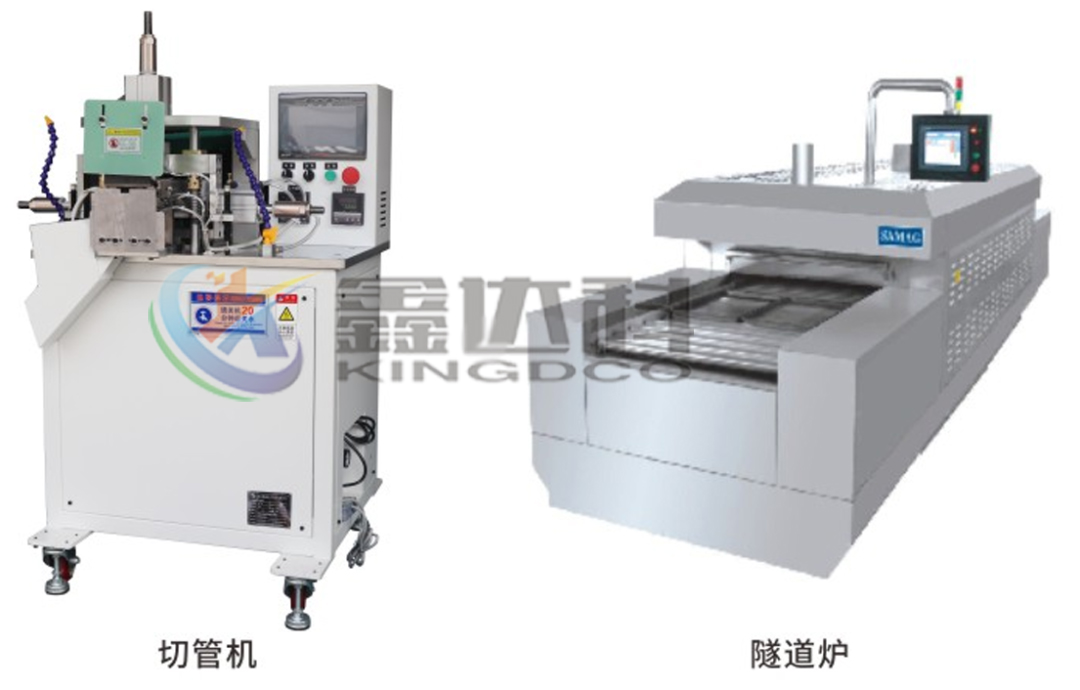
The heat shrink tubing product is flat, without damage or wrinkles, and its position is not deformed.
OP06 Bending:
The bending process relies on a bench press equipped with specialized tooling, bending and forming according to the drawing requirements, while avoiding scratching the heat-shrink insulation layer during operation;
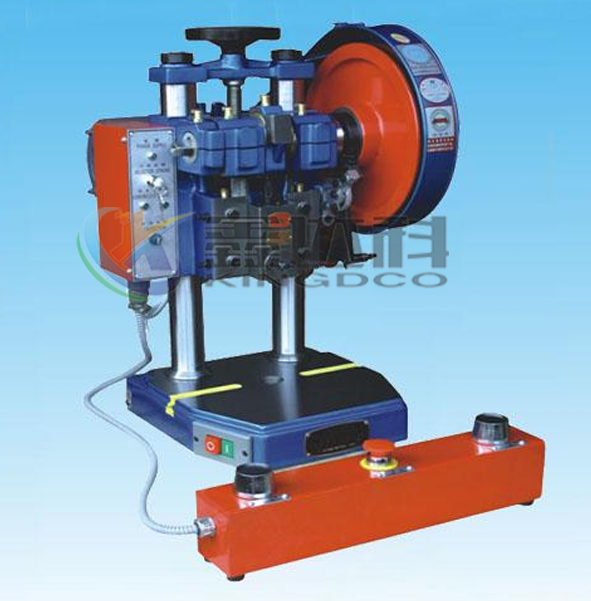
The OP05 heat shrink tubing and OP06 bending processes can be swapped according to product requirements. The cycle time of these two processes varies with product length and bending complexity, ranging from 5 to 60 seconds.
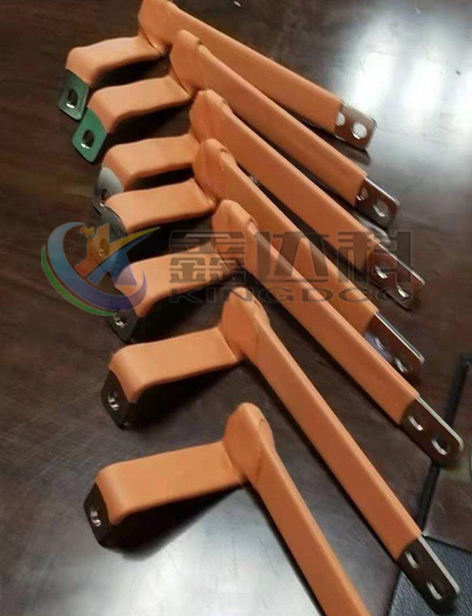
OP07 Finished Product Inspection:
Finished product inspection is a key link in quality control, equipped with pull force testers, vibration testers, contact resistance testers, temperature rise testers, flame retardant testers, and other testing equipment;
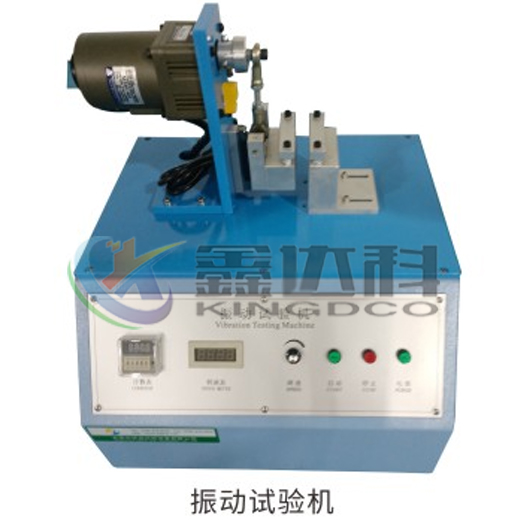
Check the welding flatness and insulation integrity one by one, while simultaneously carrying out tensile tests, fatigue tests, current tests, resistance tests, temperature rise tests, flame retardant tests, etc., and separately store the NG products. The inspection cycle is 5~100 seconds.
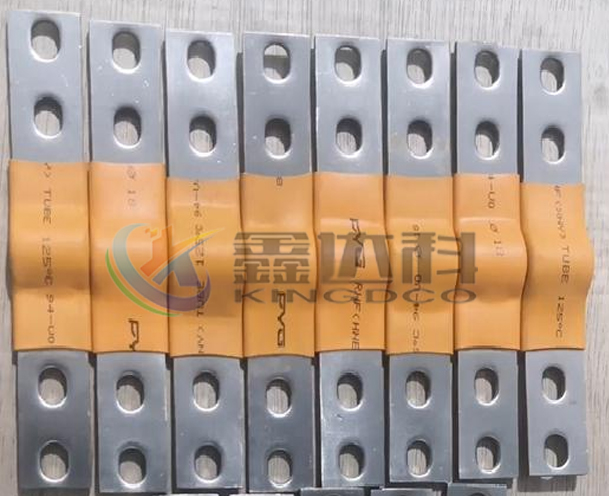
OP08 Packaging Station:
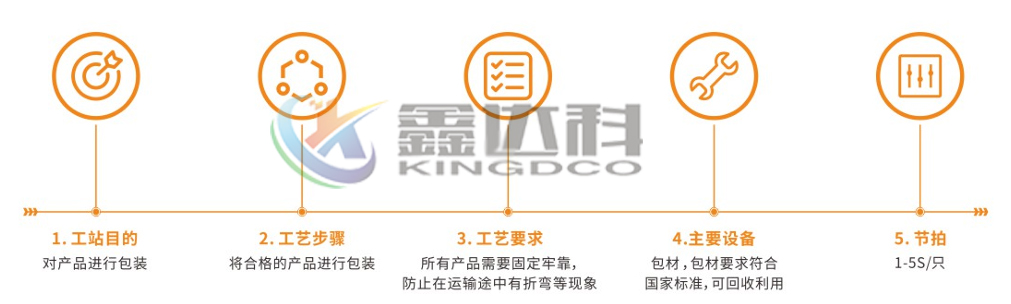
Package the qualified products according to standards, secure them with protection to prevent bending during transportation, cycle time 1~5 seconds.
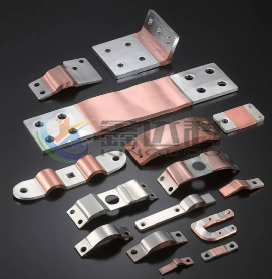
Copper and aluminum busbars are widely used in battery packs. Nowadays, the busbars are mostly made of multilayer copper foil/aluminum foil laminates as the base material, and are fabricated through a...
2026-08-05 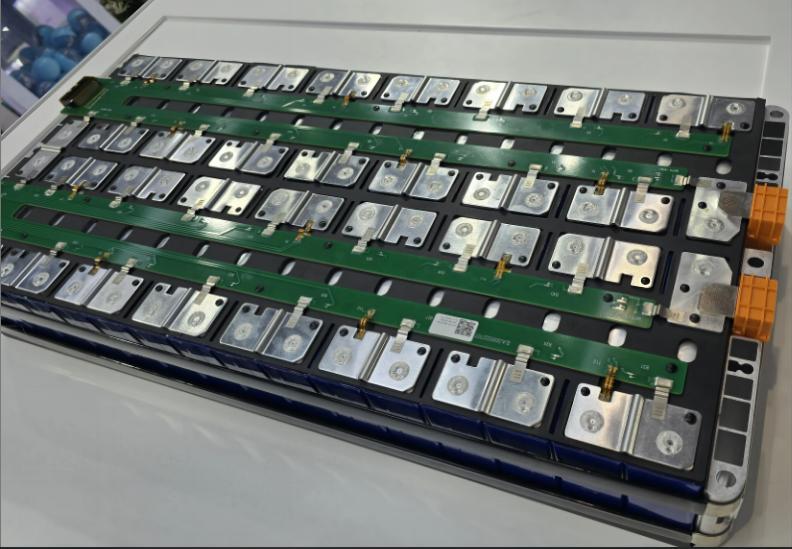
The CCS integrated busbar is mainly composed of signal acquisition components (such as FPC, PCB, FFC, etc.), plastic structural parts, nickel strips, copper busbars, aluminum busbars, etc. These are c...
2025-08-15 
Nickel is a metal with significant industrial value, with a melting point of 1453°C, a boiling point of 3075°C, and a specific gravity of 8.8 g/cm³. It has excellent corrosion resistance, is not easil...
2025-08-15 
Product Name: Power battery soft aluminum busbar, battery module welding flexible connector aluminum busbar, battery soft aluminum busbar Product Material: 1060 O-temper aluminum foil strip, aluminum ...
2023-05-04Phone:
0510-87183933